
About Awa Vinegar Brewing

Greetings
Since our founding in 1946, we have dedicated ourselves to serving as a vital link between our customers and the local community. We hope that by acting as a conduit, our local producers can share their goods with the rest of the country and prosper. We strive every day to ensure that our customers can enjoy the authentic beauty that Tokushima has to offer and find true satisfaction in our products.
In recent years, we have been actively addressing issues that affect the entire region, such as environmental concerns and an aging population, making the creation of a society that offers security and hope to the next generation our top priority. We are currently developing business initiatives with an eye toward the local community 100 years from now.
In an age filled with unsettling news, we aim to be a company that moves forward and develops alongside the community, while cherishing the traditional Japanese spirit of consideration and mindfulness.
Manabu Yoshino, Representative Director
"We will introduce the flow of a lean, systemized factory."

#1 Receiving and Inspection
All inspections are performed manually,
and the product color is checked.
We examine every single item,
carefully checking stems and sorting out smaller pieces.
In addition, we thoroughly verify
the residual pesticide checks provided by our suppliers.

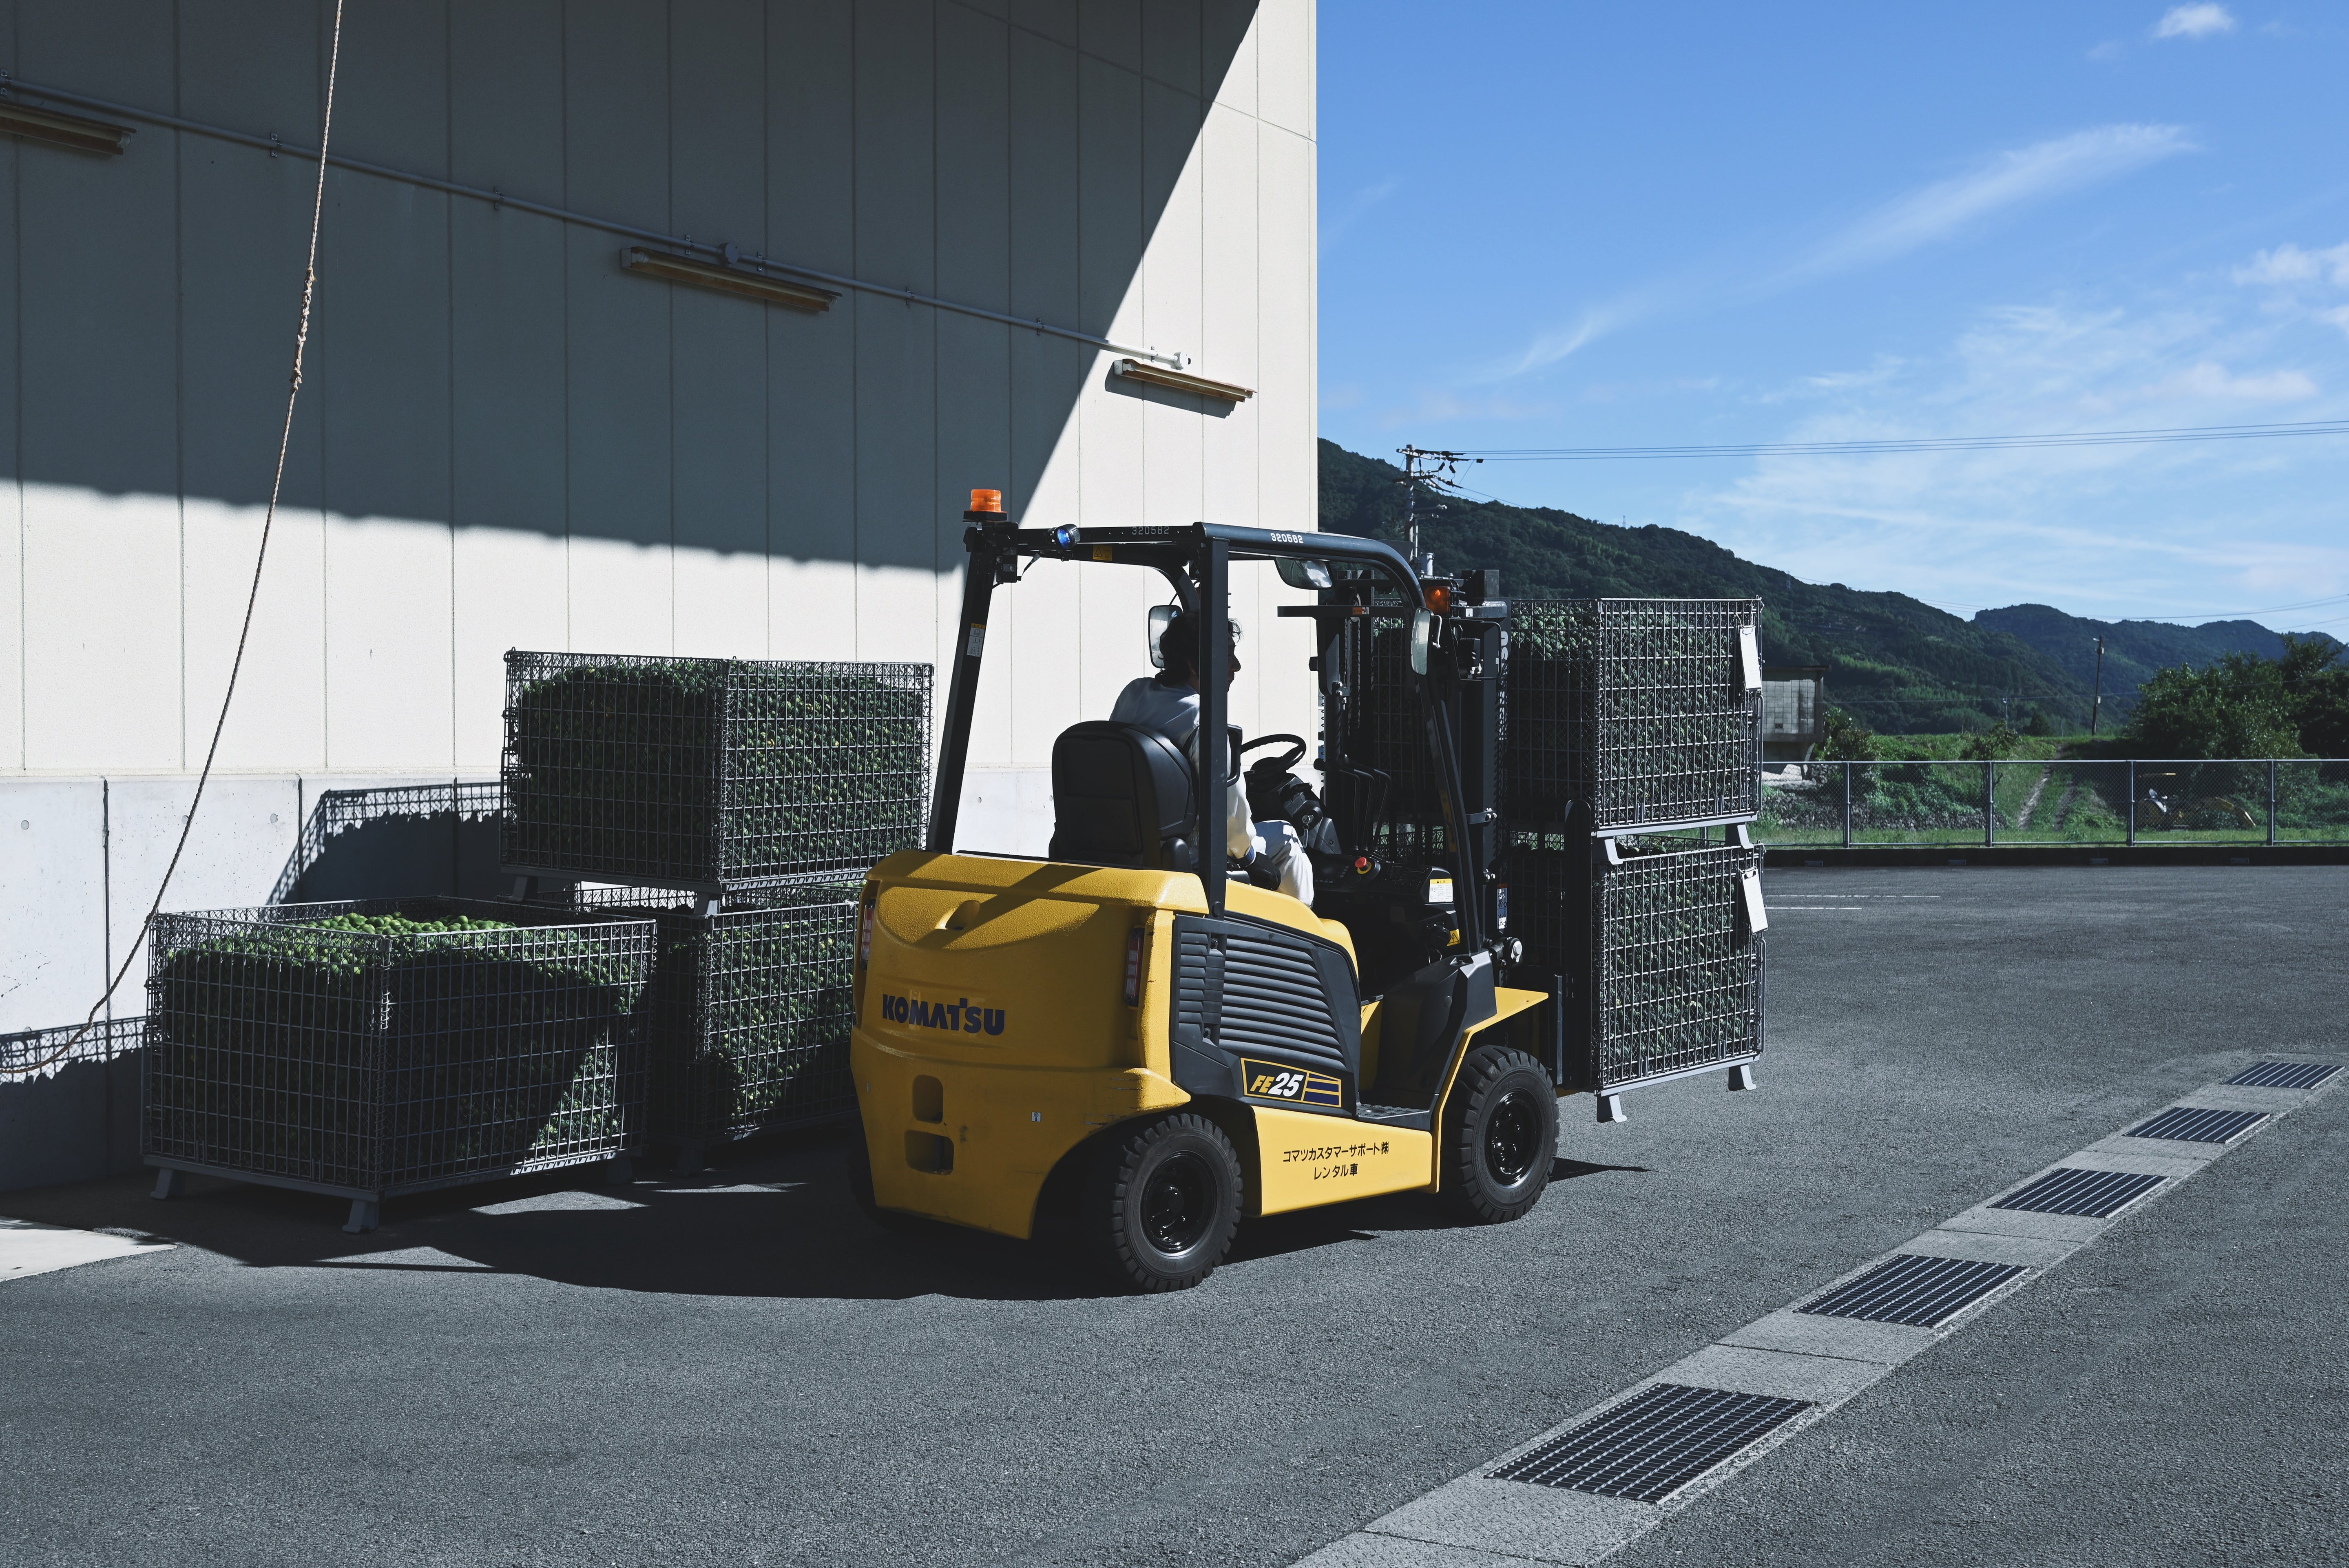
1. At our farmers in Katsuura District,
lines form for raw material deliveries when the harvest season arrives.
(Around September)

2. We also receive raw materials from JA branches and suppliers outside the town.
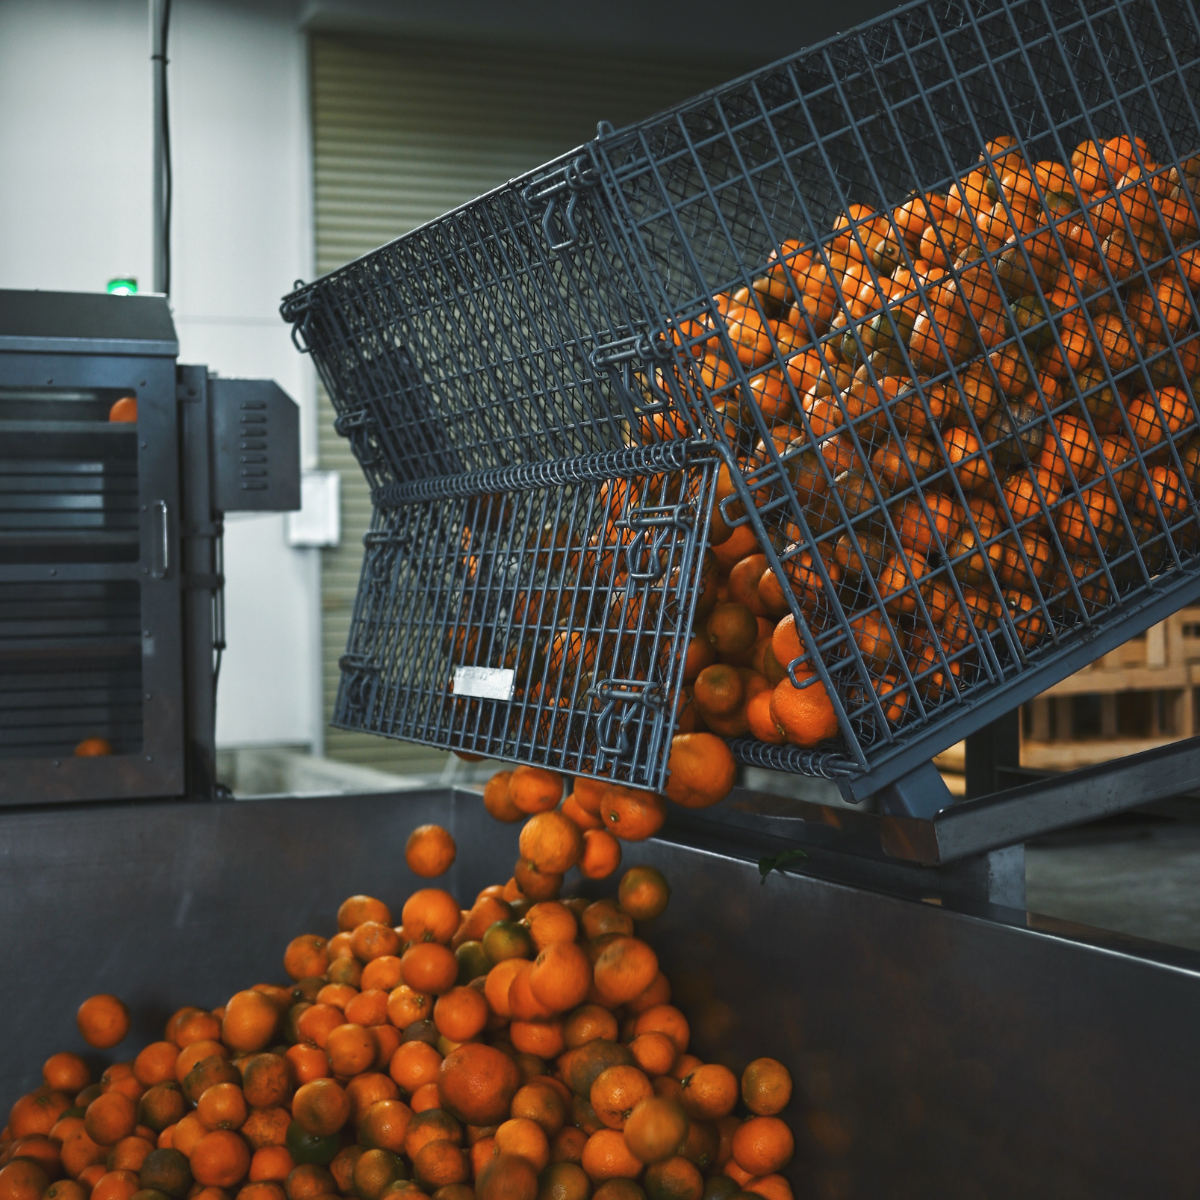
3. Fresh raw materials are dropped onto the conveyor belt.

4. The incoming raw materials are carefully inspected by hand.
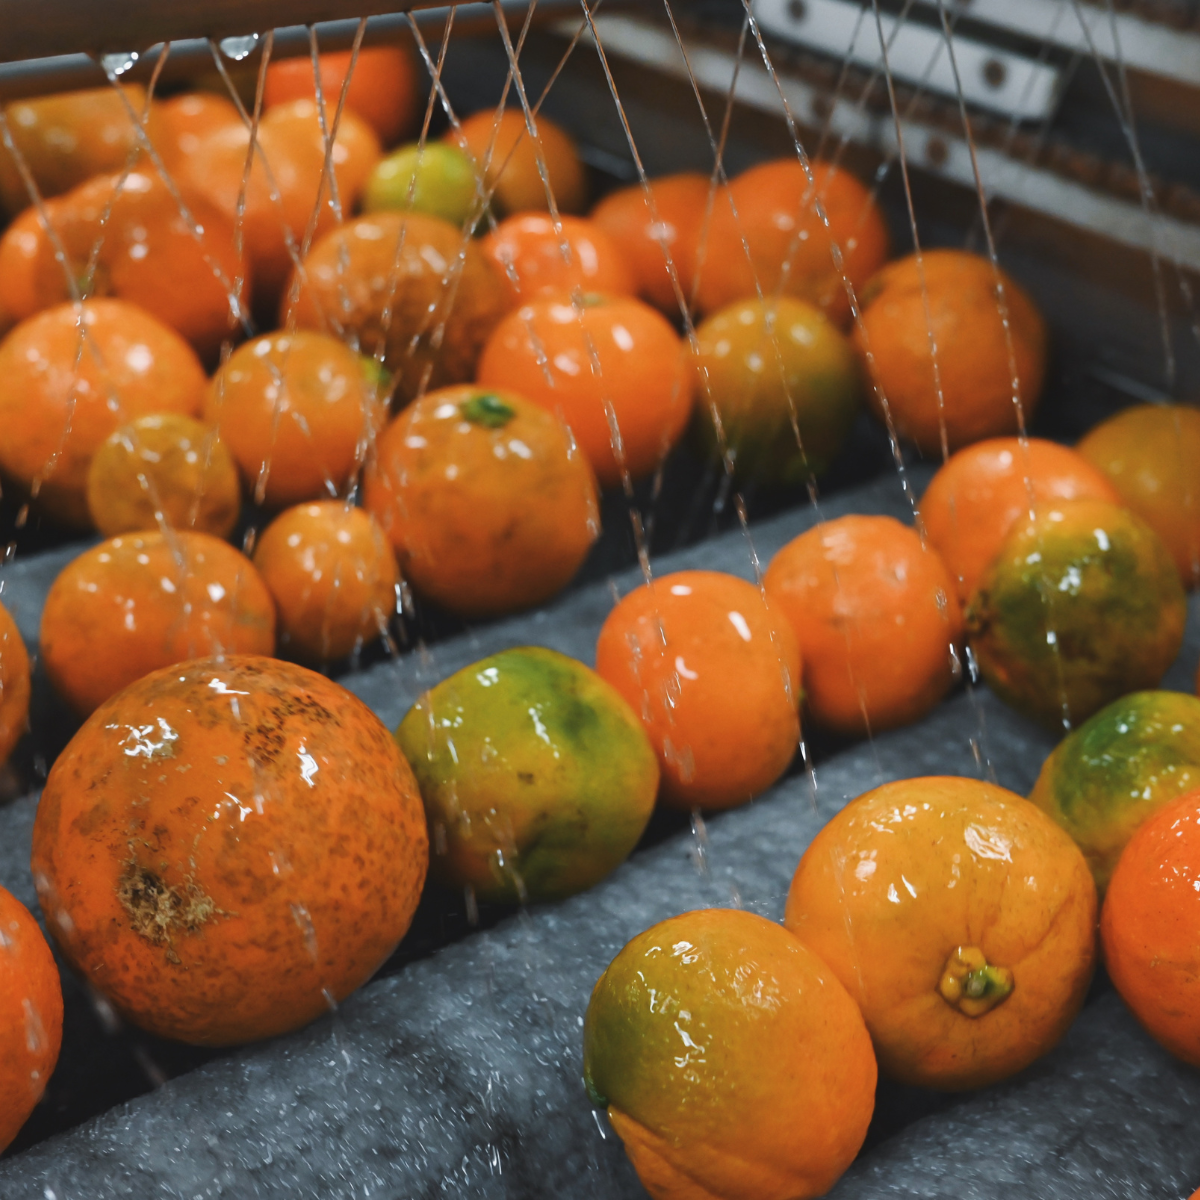
5. Once the inspection of the raw materials is complete, they are thoroughly cleaned.

#2 Squeezing and filling
In our thoroughly streamlined factory,
our specialized production lines
eliminate waste at every stage from raw material intake to final product shipment, ensuring short lead times.
Everything from the cleaning of delivered raw materials to the pressing process is systematized, and the bottles used for delivery are also thoroughly cleaned.

6. The thoroughly washed raw materials
travel along a conveyor to the juice extractor.

7. The raw ingredients are thoroughly pressed using an automatic juice extractor.

8. After pressing with a juice extractor, the juice and the peel are separated.

9. Extract the freshly squeezed fruit juice (first press).
Thorough rationalization has
achieved high quality
Our current factory, which has thoroughly rationalized the flow of its production line starting from the design phase, eliminates waste to the extreme between every process from the delivery of raw materials to the shipment of products.
We can process 50 tons of fruit per day (8-hour operation), producing 8,300 1.8L bottles of juice.
Since products are moved immediately after manufacturing to refrigerated storage on-site, we are able to maintain high quality in all of our products during storage.


Equipment overview
Juice Extractor
Juice Tank
Bag-in-Box Filler
Receiving and Sorting Equipment
Capper
Rinser
Clean Room Air Conditioner
Boiler Equipment
Peel/Pulp Separator (Rotary Slicer)
Washing and Drying Equipment
Vibrating Filter
Weigher
Filler
Cap Sorter/Feeder
Plate Pasteurizer
Cooling Unit (Cooling Unit)
Refrigerator


Contributions to the environment and local community
It is our mission as those living in the present to pass on a rich natural environment and a safe local community to future generations, and we must make careful use of limited resources and energy to reduce our environmental impact.
In Tokushima Prefecture, nearly 4,000 tons of "pulp residue" are generated annually during fruit juice extraction, and the disposal of this waste has become a significant issue.
Our company was one of the first in the prefecture to address this problem, launching a business to produce compost using this pulp residue as a raw material.
We transport the fruit pulp residue remaining after juice extraction to our own compost facility to manufacture and sell our organic fertilizer, "Super Green."
The compost we produce is returned to local farmers, who use it to grow even better fruit and crops, creating a sustainable cycle.
Currently, with an aging farming population and a declining birthrate in the local area, the local farmers appreciate the market we provide for processing-grade fruit (used for fruit vinegar), which can be produced with less labor.
ABOUT US
Company Profile
【Company Name】
Awa Suzo Co., Ltd.
【Address】
52-1 Kamino-ki, Oaza-Ikuna, Katsuura-cho, Katsuura-gun, Tokushima 771-4303
TEL: 0885-42-2800 (Main)
FAX: 0885-42-2600
【Representative】
Manabu Yoshino, President and Representative Director
【Founded】
January 1946
【Established】
January 1971
【Capital】
10 million yen
【Banks】
The Awa Bank, The Tokushima Taisho Bank, Mizuho Bank, The Shikoku Bank
【Business Activities】
Manufacturing and sales of fruit vinegar (sudachi, yuzu, yukou juice, and bitter orange juice), manufacturing and sales of organic fertilizer
【Land Area】
5,280㎡
【Building Area】
[Factory] Steel structure, 2 stories, 1,650㎡ total floor area
[Refrigeration Building] Steel structure, 1 story, 330㎡ total floor area
Capacity to keep 100,000 bottles (1.8L bottles) refrigerated
【Manufacturing Plant】
7 Ota, Oaza-Ikuna, Katsuura-cho, Katsuura-gun, Tokushima
【March 1946 (Showa 21)】
Kohei Yoshino founded the business as a citrus wholesaler.
【September 1950 (Showa 25)】
Began manual squeezing of sudachi, yuzu, and yukou citrus fruits.
【January 1971 (Showa 46)】
Established Kanekichi Sangyo Co., Ltd.
(Fruit vinegar manufacturing/sales division, fuel sales division)
【May 1972 (Showa 47)】
Constructed a citrus juice extraction plant.
【November 1981 (Showa 56)】
Completed small-bottle filling facilities.
(Began nationwide rollout of sudachi and yuzu vinegars in small bottles, in addition to standard 1.8L bottles.)
【May 1983 (Showa 58)】
Began manufacturing and sales of "Manyo no Sei / Sudachi Honey and Yuzu Honey,"
additive-free, ready-to-dilute healthy beverages.
【August 1986 (Showa 61)】
Constructed a second citrus plant.
(Equipped with five juice extractors.)
【February 1991 (Heisei 3)】
Manabu Yoshino appointed as Representative Director.
Established Awa Suzo Co., Ltd. as a sales company.
【August 1991 (Heisei 3)】
Constructed refrigeration facilities.
(Ensured strict quality control by refrigerating juice immediately after extraction.)
【August 1994 (Heisei 6)】
Constructed a second refrigeration facility.
【April 2001 (Heisei 13)】
Constructed a compost facility.
(Built to proactively address environmental issues regarding citrus pulp disposal by recycling the pulp into compost.)
Began manufacturing and sales of "Super Green,"
a compost made from recycled citrus pulp.
【November 2003 (Heisei 15)】
Obtained organic certified factory status from the NPO Tokushima Organic Agricultural Products Certification Association.
(As Kanekichi Sangyo Co., Ltd.)
【August 2005 (Heisei 17)】
Relocated the head office plant to Shinjinoki, Oaza-Ikuina, Katsuura-cho.
(Equipped with clean rooms to dedicate efforts to safe and secure product manufacturing.)
【February 2006 (Heisei 18)】
Began juice extraction of daidai (bitter orange).
Began manufacturing and sales of Manyo no Sei / Daidai Honey.
【May 2009 (Heisei 21)】
Unified the company name to Awa Suzo Co., Ltd.,
focusing exclusively on the fruit vinegar manufacturing and sales division.
【January 2014 (Heisei 26)】
Obtained organic certified factory status from the NPO Tokushima Organic Agricultural Products Certification Association.
(As Awa Suzo Co., Ltd.)
【November 2018 (Heisei 30)】
Received the Tokushima Prefectural Governor's Award.
(As an excellent food hygiene facility.)
【March 2020 (Reiwa 2)】
Obtained Tokushima Prefecture HACCP certification.